How to Evaluate Factory Supplier Capability Before Shortlisting Vendors?
Shortlisting a factory on price sheets and sample photos alone creates avoidable risk. A sound supplier capability evaluation for factories starts with one practical question: can this site repeatedly deliver the exact material, finish, tolerance, packaging, and lead time required under normal production pressure? If the answer is unclear, the vendor is not ready for a shortlist, no matter how polished the presentation looks.
The first useful signal is production fit. A capable factory may still be a poor match if its main line, tooling logic, or material flow was built for products unlike yours. Ceramic tile plants, sheet metal workshops, faucet assemblers, sanitary ware manufacturers, cabinet fabricators, and smart hardware lines all have very different bottlenecks. The review should therefore begin with product family alignment: substrate type, thickness range, surface treatment, dimensional control, joining method, moisture exposure, installation environment, and expected service life. A plant that usually runs standard indoor decorative panels may struggle with exterior-grade boards, wet-area sealing details, or repeated color consistency across multiple batches.
Ask for a live explanation of the process route rather than a general brochure. The useful version is specific: incoming material inspection, cutting or forming, edge processing, drilling, welding or bonding, coating or glazing, curing, calibration, final assembly, testing, packing, and shipment release. When a factory cannot describe where defects are most likely to occur in its own process, it usually means controls are reactive rather than built into production.
Read capability through the production floor, not the sales deck
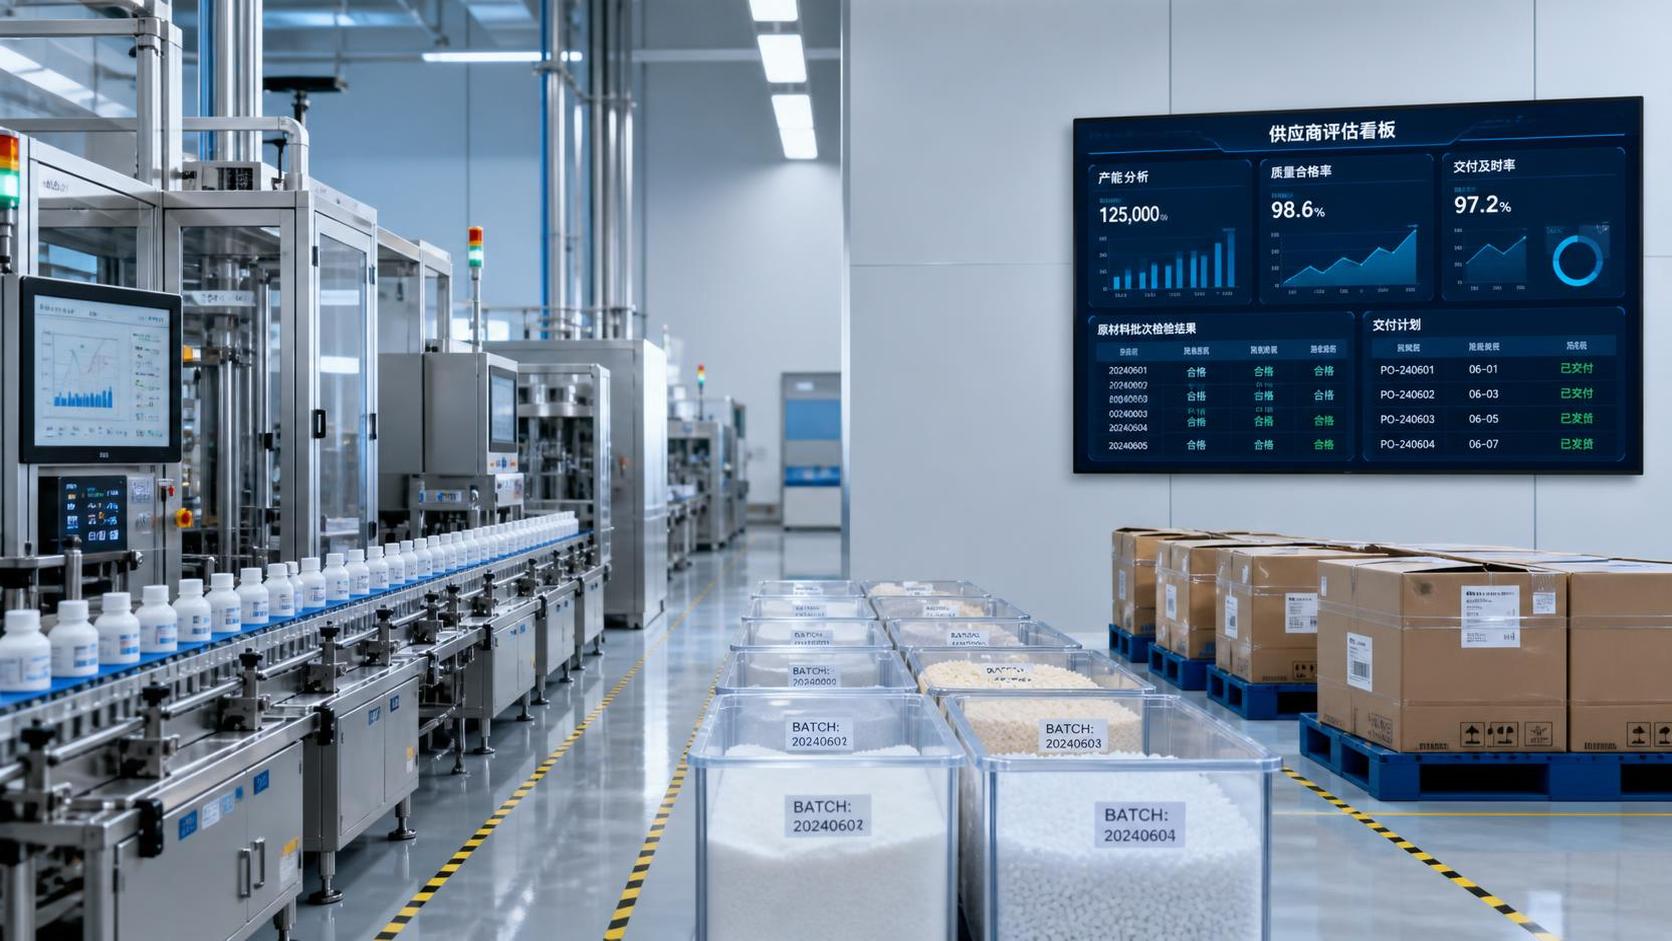
A site visit, whether physical or remote, should focus on flow and discipline. Look for whether materials are identified by batch, whether work-in-progress is separated clearly, and whether rejected items are physically isolated instead of mixed back into the line. A factory that keeps similar finishes or hardware variants side by side without robust labeling may create picking errors later, especially in mixed project orders with many SKUs.
Machine count is less important than machine suitability and condition. A supplier may show a long equipment list, but the relevant points are narrower: are the machines compatible with the required dimensions and tolerances, are maintenance records current, and is there enough process stability to avoid manual correction at every stage? Repeated hand rework around edge trimming, hole position correction, polishing, or fit-up often signals weak upstream control. That pattern tends to expand lead time and quality variation at the same time.
Capacity claims deserve pressure testing. Instead of asking for total monthly output, ask how much output is realistically available for your product type during peak periods, how many shifts are normal, what changeover time is needed between finishes or models, and which step becomes the constraint first. In architectural materials, the bottleneck may sit at kiln time, coating cure time, polishing, CNC availability, or final inspection benches rather than at the earliest machining stage. If that constraint is already fully loaded, nominal capacity is meaningless.
Material control usually predicts downstream quality
Many supplier failures begin before production starts. Resin grade, alloy composition, clay body stability, stainless thickness, chip origin, seal material, hinge hardness, and coating chemistry all influence the final result, yet some factories inspect only visible damage on arrival. Strong factories can explain what they verify when raw materials enter the site, how lots are recorded, and what happens when a batch falls outside target range.
For building products and sanitary components, traceability matters because defects often appear after installation rather than at dispatch. Warpage, color drift, poor glaze adhesion, rust bleed, swelling near wet edges, leaking joints, unstable sensor response, and premature coating failure may trace back to one incoming batch. A supplier that cannot connect finished goods to material lots will struggle to isolate the issue without freezing large amounts of stock.
Material substitution is another fault line. Some factories substitute adhesives, core boards, fasteners, valves, cartridges, gaskets, or packaging inserts when supply tightens. That is not always unacceptable, but it must be controlled and disclosed before shipment, especially when the product will be installed in humid spaces, subject to cleaning chemicals, or connected to water systems. Silent substitution is a disqualifying sign during evaluation because it breaks specification discipline.
Sample quality only matters if it can be repeated at production scale
A polished pre-production sample proves very little on its own. Samples are often handled by the most experienced technician with extra time and selective material choice. The more reliable test is whether the supplier can define the sample standard in measurable terms and replicate it across a batch. Surface gloss, joint gap, edge straightness, dimensional variance, mounting hole position, coating thickness, opening force, flushness, drainage slope, and color continuity should be translated into approved references or tolerances before a factory reaches the shortlist.
It is also worth asking how the factory controls visual standards when products are judged under different lighting conditions. This matters in tiles, decorative metals, engineered stone, cabinetry fronts, and bathroom fittings where color or texture variation becomes visible only after installation across a large area. A supplier may ship pieces that pass one-by-one inspection but still look inconsistent once installed side by side. Capability evaluation should therefore include batch-level visual control, not only piece-level acceptance.
Engineering response speed is part of capability
Factory strength is not only about making the current drawing. It includes how the team handles revisions, conflicts, and ambiguous details. During evaluation, send a controlled set of technical questions: a corner condition, a tolerance stack-up issue, an interface with another trade, a packaging challenge, or a request for alternate material under the same performance need. The response should show process understanding, not generic reassurance.
Good engineering support often reveals itself in the questions the supplier asks back. If the factory asks about substrate condition, wall flatness, expansion allowance, fixing method, water exposure, transport orientation, or installation sequence, that is generally a positive sign. It shows the plant understands that product quality depends on application conditions, not just manufacturing drawings. A factory that accepts every drawing without comment may simply be pushing technical risk downstream.
For products involving electronics or smart components, capability evaluation should include firmware control, component version tracking, test coverage after assembly, and replacement logic for failed modules. A neat housing and clean finish do not compensate for weak control of sensors, power units, connectors, or communication modules. Even when the sourcing scope is mainly architectural, these details matter once smart locks, touch controls, or water-management features are included.
Quality systems should be visible in daily behavior
Formal documents have value, but behavior on the floor reveals more. Look for whether inspection criteria are available at the workstation, whether gauges are calibrated and actually used, whether first-off approval exists after setup changes, and whether operators can stop a batch when they see drift. If defect handling depends on a supervisor noticing problems at the very end, the system is too late.
Nonconformance handling is especially telling. Ask the factory to describe a recent internal defect and how it was contained. A credible answer usually includes segregation, root-cause review, corrective action on process settings or tooling, and a method to prevent recurrence. Weak answers stay at the level of “workers were reminded to be careful.” That suggests the problem is treated as human error even when the real cause may be unstable process design.
Packaging control belongs in the same conversation. Many technically acceptable products fail after production because corners crush, polished faces abrade, labels detach, moisture enters cartons, or mixed hardware bags are packed incorrectly. In cross-border trade, the packaging system should match route length, handling frequency, stacking pressure, and climate exposure. A supplier with strong manufacturing and poor packing discipline can still create site rejection and replacement delays.
Lead time reliability depends on planning maturity
Factories often quote lead time as a sales commitment rather than a schedule built from real planning logic. During evaluation, ask how orders are slotted, how material availability is linked to the plan, what happens if one upstream material is delayed, and whether project orders are split by line, color, or final destination. A reliable answer includes sequence logic and escalation points, not a simple promise to expedite.
Where multiple subcontracted steps are involved, such as anodizing, tempering, glazing decoration, outsourced PCB loading, or specialized surface treatment, the evaluation should map those dependencies clearly. A factory may appear integrated but still rely on outside partners for the very step that defines appearance or performance. That is not automatically negative, yet it changes risk. The shortlist should reflect whether those outsourced stages are controlled through fixed standards, approval samples, and realistic transport timing between facilities.
Commercial discipline affects operational stability
Commercial terms can expose hidden operational weakness. If a supplier resists documenting revision control, packaging standards, spare-part scope, or claim handling boundaries, the issue may not be legal caution alone. It may indicate that internal execution is inconsistent. A factory that is genuinely in control usually prefers clarity because it reduces later disputes over finish acceptance, quantity variance, accessory inclusion, and replacement responsibility.
Another useful test is document consistency. Compare the quotation, technical sheet, drawing notes, sample label, packing list format, and correspondence language. Misalignment across these documents often predicts errors during mass production. If the finish code changes from one file to another, if dimensions are quoted in mixed conventions, or if optional accessories are described ambiguously, the shortlist decision should pause until the supplier shows tighter control.
Common false positives during shortlisting
- A large site with many machines may still have poor process control for custom or mixed-batch work.
- Fast sample turnaround can hide the fact that the plant used manual intervention that does not scale to production.
- Low defect claims in conversation are not persuasive if traceability, quarantine practice, and failure records cannot be shown.
- Clean showrooms and export packaging mockups do not prove material stability under moisture, load, abrasion, or repeated use.
- Strong communication from sales staff may mask slow engineering feedback or overloaded production scheduling.
A practical shortlisting decision usually becomes clearer when all findings are converted into a small comparison frame: product fit, process maturity, material control, repeatability of sample quality, engineering responsiveness, planning reliability, packaging discipline, and transparency around constraints. The strongest factories are not the ones claiming perfection. They are the ones that can define their operating limits, explain their controls in detail, and show that quality survives beyond the sample room and into normal production conditions.
Industry Briefing
Get the top 5 industry headlines delivered to your inbox every morning.